Test matrix
List products, bottles, caps, labels, packs, formats, recipes, speeds, run periods, changeovers, cleaning or sanitation functions and abnormal conditions included at each stage.
Factory planning for water bottling projects
Use two tests to prove different project questions
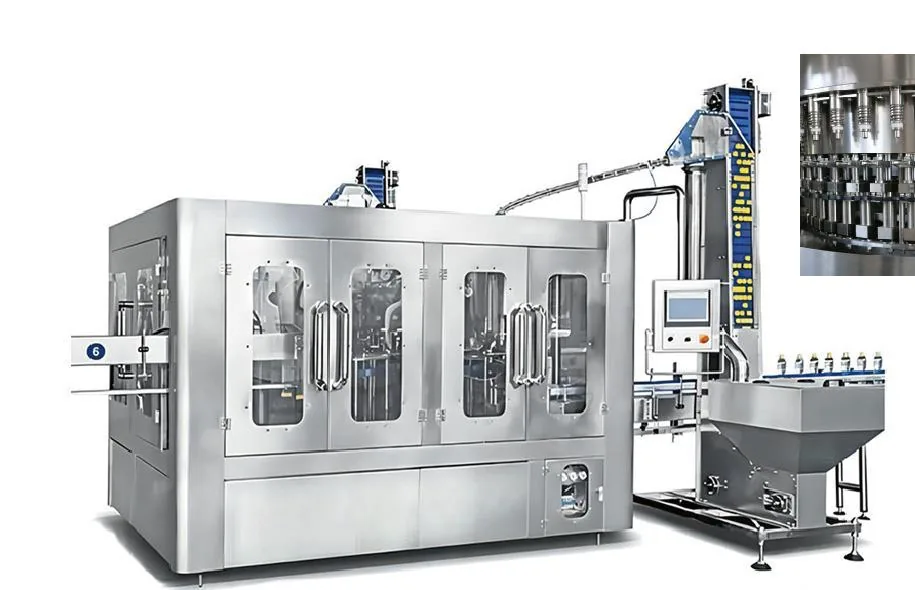
Factory acceptance testing and site acceptance testing are not duplicate runs in different locations. FAT examines agreed equipment and functions before shipment under the factory conditions that can be provided. SAT examines the installed system with real site utilities, connections, materials, operators and surrounding equipment. The contract should define how evidence, deviations and open actions move between both stages so shipment does not erase unresolved work and site testing does not repeat undefined expectations.
01
A clear boundary prevents both tests from becoming informal demonstrations.
| Question | FAT focus | SAT focus | Document that connects them |
|---|---|---|---|
| Equipment supplied | Identity, build, functions, safety and documents available before shipment | Installed identity, condition and completed field work | Equipment list and inspection record |
| Interfaces | Simulated or factory-provided signals, materials and utilities | Actual site utilities, connections and adjacent systems | Interface schedule and responsibility matrix |
| Performance | Agreed factory condition and available representative materials | Agreed installed-line condition with site materials and operators | Acceptance procedure and data sheet |
| Completion | Shipment release and recorded open actions | Final closure, training and operating handover | Punch list and handover register |
02
The result is only meaningful when product, materials, duration and measurement are agreed.
List products, bottles, caps, labels, packs, formats, recipes, speeds, run periods, changeovers, cleaning or sanitation functions and abnormal conditions included at each stage.
Name who provides materials, utilities, instruments, operators, local labor, lifting, network access and waste handling. Confirm readiness by a defined date to avoid testing on substitutes without approval.
Define counters, quality checks, stop classification, sampling, data sheets, permitted exclusions, witnesses and the decision authority. Avoid relying on a catalog rate without agreed operating conditions.
03
The project needs continuity, not two disconnected reports.
Capture configuration, software version, materials, conditions, results, observations, deviations, photographs or video where agreed and the signed decision for shipment.
Record disassembly, preservation, transport damage, field modification, software or component replacement and reassembly checks that could affect the factory result.
Classify each action, owner, due date, evidence and whether it blocks shipment, energization, product trial, acceptance or handover. Closure should require the agreed evidence, not only a status message.
04
Site acceptance should prove the installed boundary and leave the plant able to operate and maintain it.
Progress through installation checks, dry functions, utilities, water, product, connected-line balance and agreed performance without skipping prerequisites.
Include buyer operators and maintenance roles, approved procedures, quality checks, recipes, backups, manuals, spares, training records and safe restart or fault-recovery practice.
Record accepted scope, outstanding non-blocking items, warranty or service start basis where contracted, document status and responsibility for remaining work. Do not present SAT as local statutory approval.
Buyer questions
No. FAT cannot prove the final building, utilities, local connections, installation, adjacent systems, site materials and operating team.
Only under the agreed decision process. Actions should be classified with owner, due date, evidence and impact on shipment and later gates.
The contract and test plan should name the source, quantity, approval status, delivery date and responsibility for representative materials at each test.
No. SAT is contractual technical evidence for the agreed project boundary; local product, building, safety and regulatory approvals remain separate responsibilities.
Move this project question forward
The project needs continuity, not two disconnected reports.
Not sure which data matters? Send what you have and state the decision you need to make.
Send target capacity and SKUs, source-water report, site utility schedule, building layout and required project milestones.
The project desk can identify missing inputs and a practical next step. Final engineering, configuration, compliance and commercial terms remain project-specific.
Allot Tech (Suzhou) Co., Ltd. · sales@allottech.com · Project telephone: +86 186 6213 1120 / +1 818 262 0958