Reference bottle
State which bottle volume and design the target applies to. Larger or unstable containers may have different handling and achievable speeds.
Factory planning for water bottling projects
Startup scale without an incomplete factory
A 2,000-bottle-per-hour planning target can support a controlled market entry, but the right configuration depends on bottle formats, daily volume, labor, utilities and whether bottles are purchased or produced on site.
01
The capacity label needs an operating basis before it can guide equipment selection.
State which bottle volume and design the target applies to. Larger or unstable containers may have different handling and achievable speeds.
Convert saleable demand into scheduled days, shifts and hours, then allow for cleaning, changeover, maintenance and startup learning.
List each bottle, cap, label and pack expected at launch so change parts and manual tasks are visible.
Decide what measured demand or utilization level justifies extra shifts, more automation or a higher-capacity line.
02
At this scale, labor and local bottle supply can materially change the best solution.
| Decision | Possible route | What to verify |
|---|---|---|
| Bottle supply | Purchase approved empty bottles | Quality consistency, transport damage, storage volume and hygienic handling |
| Bottle production | Blow preforms in house | Molds, high-pressure air, cooling, power, operators and maintenance |
| Packing | Manual, semi-automatic or automatic | Labor rate, pack consistency, floor space and required shift output |
| Material movement | Manual pallet handling or conveyors | Safety, accumulation, warehouse route and expansion compatibility |
03
A small line still needs all functions required to produce, check and dispatch saleable packs.
Design from actual raw-water analysis and product requirements, with tanks, sanitation, sampling and a stable transfer to filling.
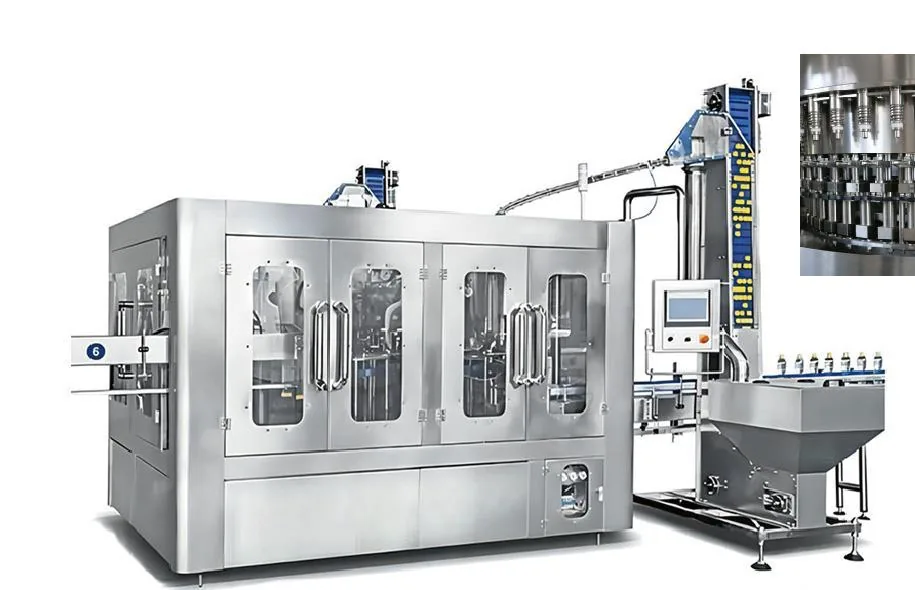
Define rinsing, filling, capping, cap supply, product-contact boundary, drainage, controls and the reference formats.
Confirm label technology, coding, pack pattern, rejected-pack handling and how finished packs reach pallets or storage.
Prepare power, air, water, drains, cooling where required, testing, records, spares and trained operating roles.
04
Expansion is easier when the first project leaves usable interfaces.
Review whether selected capacities and connection points can support longer hours or the next line stage.
Keep an expansion direction and service routes clear of permanent obstructions where the site allows.
Identify which coding, inspection, treatment or packing modules can remain and which would become a constraint.
Avoid assuming future integration; document the available signals, speeds and mechanical interfaces.
05
These figures are arithmetic planning examples, not promised output. Utilization combines scheduled time and operating losses for comparison; final saleable output depends on the confirmed bottle, materials, connected equipment, quality results and acceptance conditions.
| Illustrative schedule | Theoretical bottles | At 65% planning utilization | At 75% planning utilization | At 85% planning utilization |
|---|---|---|---|---|
| 8 scheduled hours | 16,000 | 10,400 | 12,000 | 13,600 |
| 16 scheduled hours | 32,000 | 20,800 | 24,000 | 27,200 |
Buyer questions
No. It may be too large or too small depending on demand, operating hours, format mix, inventory and distribution. Calculate capacity from the business and operating plan.
Not necessarily. Compare purchased-bottle quality, transport and storage with the investment, utilities and skills required for in-house blowing.
Staffing depends on automation, material supply, packing, sanitation, quality checks, warehouse movement and shift organization. Confirm tasks rather than using a universal headcount.
Only within confirmed machine, format and line-balance limits. A future capacity increase may require new machines, conveyors, utilities or a second shift.
For an illustrative 8-hour schedule, 2000 rated BPH equals 16,000 theoretical bottles. At 75% planning utilization the arithmetic result is 12,000 bottles before any separate quality loss assumption. Project performance must be confirmed for the selected format and conditions.
Move this project question forward
A small line still needs all functions required to produce, check and dispatch saleable packs.
Not sure which data matters? Send what you have and state the decision you need to make.
Send target capacity and SKUs, source-water report, site utility schedule, building layout and required project milestones.
The project desk can identify missing inputs and a practical next step. Final engineering, configuration, compliance and commercial terms remain project-specific.
Allot Tech (Suzhou) Co., Ltd. · sales@allottech.com · Project telephone: +86 186 6213 1120 / +1 818 262 0958